Production of Laccase Enzyme: Laccase Specification Checklist for Industrial Buyers
Compare laccase enzyme production routes, specs, QC, pilot validation, and cost-in-use for wastewater, pulp bleaching, and lignin applications.
Choosing a laccase supplier is not only about activity units. Industrial buyers should compare strain route, fermentation control, purification level, formulation stability, and performance in the real process stream. This guide folds in our earlier pages on laccase production routes and bacterial laccase; for bulk supply, send the application, grade, quantity and destination for a quote.
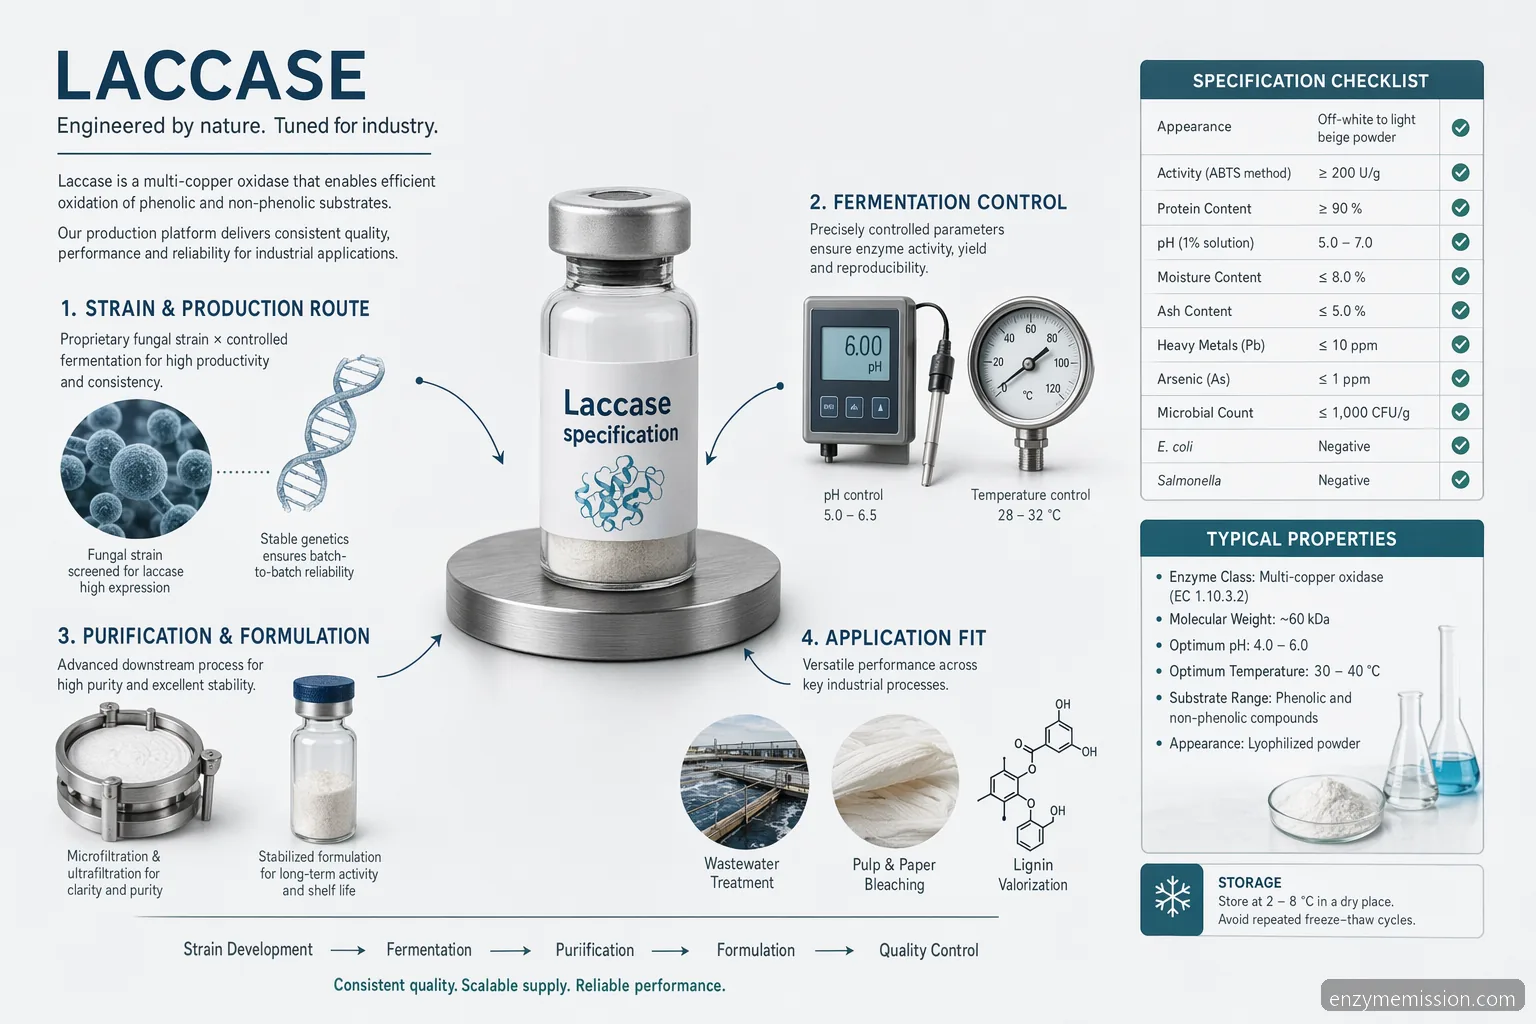
How to Compare Laccase Production Routes
The production of laccase enzyme can use fungal or bacterial fermentation, and each route affects specification strategy. Production and purification of laccase enzyme through fungi is widely studied because many white-rot fungi secrete extracellular laccase suited to lignin modification, pulp bleaching, dye decolorization, and phenolic wastewater treatment. Laccase enzyme production from bacteria may offer advantages in tolerance to pH, salinity, and temperature, depending on the strain and expression system. For B2B procurement, the best route is the one that matches your process window, not the one with the highest catalog activity. Ask suppliers to define the organism class, fermentation type, assay substrate, unit definition, carrier system, and formulation. If you are reviewing a laccase enzyme production ppt or laccase enzyme production pdf, verify that the data came from industrially relevant feedstocks and not only clean laboratory buffers.
Compare fungal versus bacterial laccase under your real pH, temperature, and contaminants. • Check whether activity is reported on ABTS, guaiacol, syringaldazine, or another substrate. • Confirm the unit definition, dilution factor, and assay temperature.
Bacterial Versus Fungal Laccase Production
Laccase enzyme production from fungi is well established and can deliver high activity under acidic conditions, especially for lignocellulosic or dye-related applications. However, bacterial systems may offer advantages where process pH is neutral to alkaline, where thermal tolerance is required, or where faster growth and simpler genetic handling are useful during development. Buyers comparing laccase enzyme production from fungi with bacterial routes should avoid assuming that one source is universally better. Activity assay conditions can differ, and a high unit value in an acidic assay may not translate to alkaline wastewater or pulp conditions. Teams evaluating production and purification of laccase enzyme through fungi should request the same documentation expected for bacterial products: assay method, substrate used, unit definition, pH-temperature activity curve, stability data, and application trial results. A direct pilot comparison on the buyer’s own matrix is the most reliable decision point.
Fungal laccases are often strong candidates for acidic lignin and dye applications. • Bacterial laccases may be preferred for neutral or alkaline industrial streams. • Always compare enzymes under the intended process pH, temperature, and contact time.
Typical Fermentation and Processing Conditions
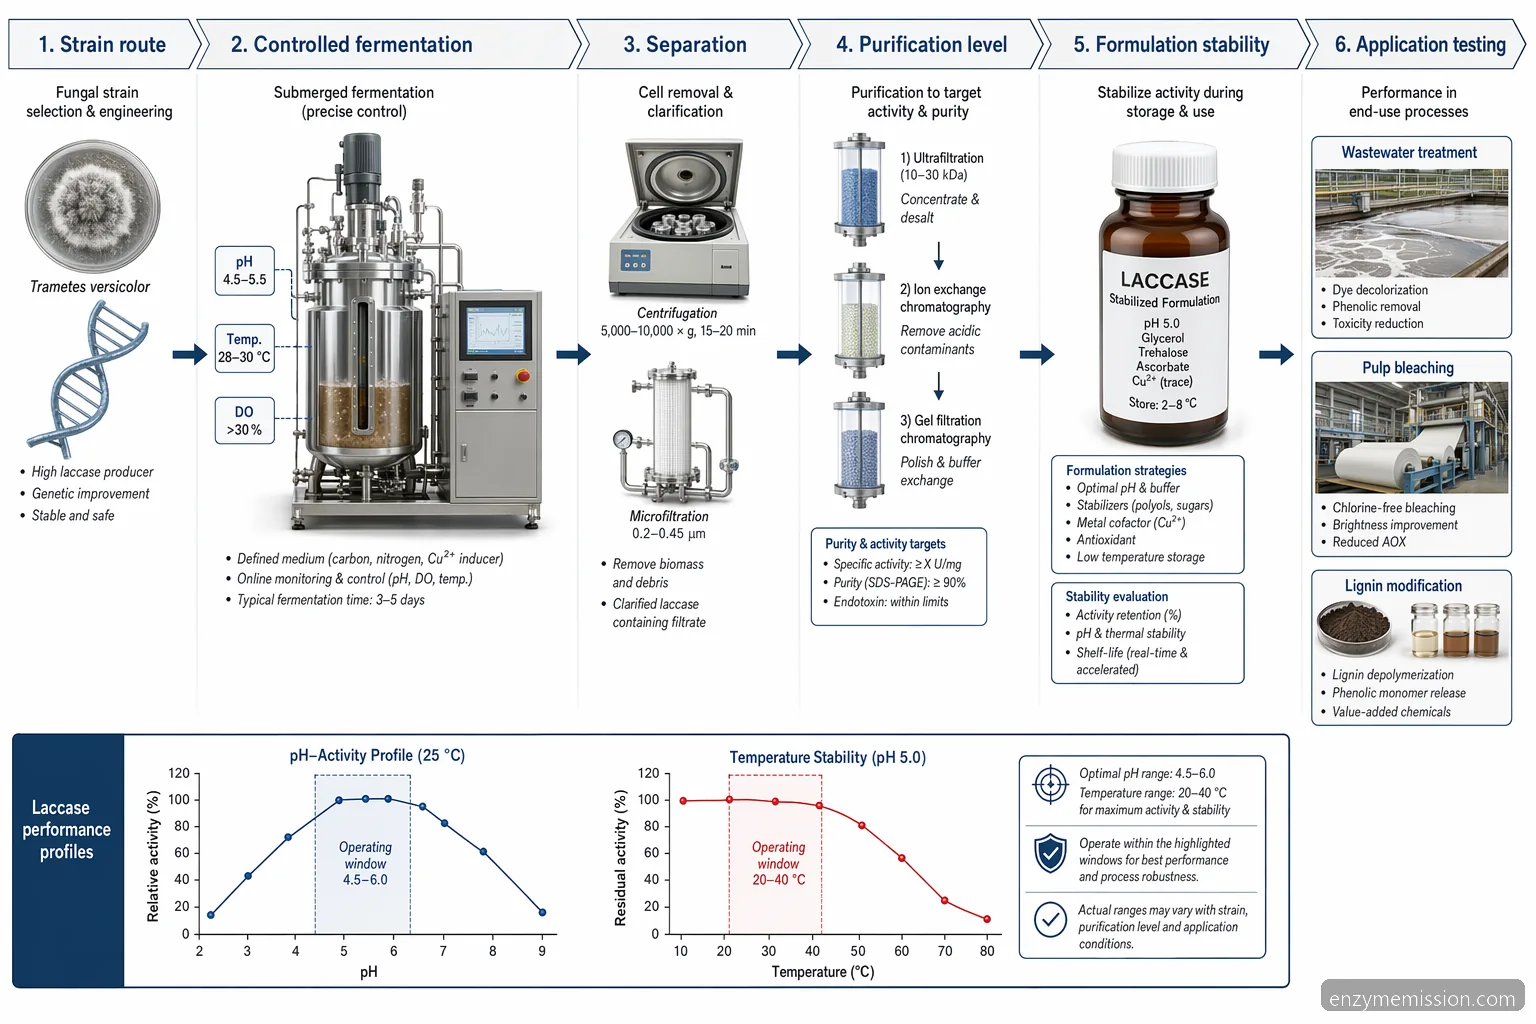
Industrial laccase enzyme production usually starts with aerobic fermentation, controlled nutrient feeding, and induction conditions optimized for enzyme expression. Fungal processes often operate around pH 4.0-6.5 and 24-32°C, while bacterial systems may be screened across pH 6.0-9.0 and 30-40°C, depending on strain tolerance. Dissolved oxygen, agitation, copper availability, carbon-to-nitrogen ratio, antifoam selection, and harvest timing can influence yield and batch consistency. After fermentation, the enzyme broth may be clarified, concentrated, filtered, stabilized, and formulated as liquid or powder. For industrial buyers, the key question is not whether laccase enzyme production is technically possible; it is whether the supplier can deliver repeatable activity, low microbial burden, stable storage, and reliable performance over multiple lots. Request trend data for activity, pH, moisture if powder, viscosity if liquid, and retained activity after storage.
Common application pH screening range: 4.0-8.5. • Common application temperature screening range: 25-60°C. • Validate stability after shipping, dilution, and process hold time.
Purification, Formulation, and QC Release
After fermentation, industrial laccase enzyme production usually moves through clarification, microfiltration or centrifugation, concentration, buffer adjustment, and stabilization. High-purity laboratory enzyme is not always necessary for wastewater treatment, pulp bleaching, or lignin modification; however, uncontrolled impurities can affect color, odor, foaming, viscosity, metal content, or downstream compatibility. A supplier should provide a Certificate of Analysis for each batch and a Technical Data Sheet that states activity, appearance, pH range, temperature range, storage conditions, and recommended handling. The Safety Data Sheet should cover workplace exposure, spill response, and transport information. Common QC checks include activity assay, protein concentration or solids, pH, moisture for powders, microbial limits where relevant, heavy metals if required by the buyer, and stability after accelerated or real-time storage. For production and industrial applications of laccase enzyme, batch consistency and application performance often matter more than a highly purified analytical profile.
Request COA, TDS, and SDS before pilot approval. • Check activity retention after storage and shipping simulation. • Match purity level to process need and budget.
Purification Level and Formulation: What Buyers Should Specify
Production and industrial applications of laccase enzyme do not always require highly purified enzyme. Wastewater treatment, bioremediation, textile effluent polishing, and pulp bleaching often use technical-grade formulations where cost-in-use is more important than electrophoretic purity. However, impurity profile still matters. Residual biomass, proteases, color bodies, salts, preservatives, and fermentation byproducts can influence odor, filterability, foaming, and compatibility with downstream equipment. A good specification should state activity per gram or milliliter, activity retention at target pH and temperature, appearance, solubility, microbial limits where relevant, heavy metal screening if needed, and recommended storage. For laccase lignin modification, buyers should also ask whether the product requires oxygen management or a mediator system. For laccase wastewater applications, ask for data on COD, color removal, phenolic reduction, sludge impact, and residual toxicity testing where applicable.
Technical grade may be appropriate for bulk industrial treatment. • Higher purification may be needed for sensitive downstream processes. • Formulation should match dosing equipment and storage conditions.
Application Fit: Wastewater, Pulp Bleaching, and Lignin
A specification checklist should be tied to the final use case. In laccase wastewater treatment, dosage may be screened from about 50-5000 U/L, depending on pollutant load, contact time, oxygen transfer, inhibitors, and mediator use. For pulp bleaching, trials commonly compare enzyme charge per oven-dry pulp, pH around 4.5-7.0, temperature around 40-60°C, and reaction time from 30-180 minutes. In laccase lignin applications, the important variables include lignin type, solids level, redox mediator, oxygen availability, viscosity, and target change such as depolymerization, grafting, or brightness improvement. Bioremediation projects should include matrix-specific inhibition testing because metals, surfactants, solvents, sulfides, and extreme pH can reduce enzyme activity. Buyers comparing laccase enzyme production from fungi with laccase enzyme production from bacteria should request side-by-side application trials rather than relying only on fermentation yield.
Screen dosage as units per liter, units per gram substrate, or units per oven-dry pulp. • Measure both enzyme activity and the process result. • Track mediator cost, oxygen demand, and contact time.
Supplier Qualification, Documentation, and Cost-in-Use
Before commercial approval, request a COA, TDS, SDS, sample retention policy, lot traceability, assay method, recommended handling, and shelf-life data. The COA should match the purchase specification, not only a generic activity number. The TDS should identify application windows, dosage guidance, compatible pH and temperature ranges, and known inhibitors. The SDS should support safe handling, storage, transport, and spill response for plant teams. Supplier qualification should include batch-to-batch comparison, pilot validation on real process material, packaging compatibility, lead time, and change-control expectations. Cost-in-use should include enzyme dose, dilution losses, storage stability, labor, mediator chemicals, aeration, reaction time, effluent savings, bleaching chemical reduction, or lignin value improvement. A lower-priced laccase enzyme may cost more if it needs higher dosage, longer contact time, or more frequent rework.
Request pilot-scale data before locking a commercial specification. • Compare cost per treated cubic meter, ton of pulp, or kilogram of lignin. • Confirm supplier support for scale-up troubleshooting.
Wholesale laccase supply and quote requests
This laccase is supplied as a dark brown powder at 1,000–10,000 U/g (ABTS assay) in 1 kg, 10 kg and 25 kg packs, with a 1 kg MOQ for trials; larger and repeat volumes are quoted per order. Resellers, distributors, treatment contractors and formulators can send the application, target stream, activity grade, quantity per order or per month, pack size and destination country to hello@mail.enzymemission.com or through the quote form. A COA is supplied for each batch.
Send: application and target stream • Send: grade, quantity and pack size • Send: destination country
Technical Buying Checklist
Buyer Questions
Fungal laccases are often extracellular and widely used in lignin, pulp, dye, and wastewater studies, while bacterial laccases may offer different tolerance profiles for pH, temperature, salinity, or inhibitors. Neither route is automatically better for every plant. Industrial buyers should compare both under real process conditions, including activity retention, impurity profile, dosage, oxygen transfer, mediator requirement, and final treatment result.
Request a COA, TDS, SDS, assay method, recommended storage conditions, shelf-life data, sample lot number, and pilot trial guidance. The COA should confirm agreed activity, appearance, formulation, and other purchase specifications. The TDS should describe pH, temperature, dosage, compatibility, and inhibitors. The SDS helps site teams evaluate handling, PPE, storage, and spill response before the enzyme enters production.
Cost-in-use should be calculated per cubic meter treated or per kilogram of pollutant reduction, not only by enzyme purchase price. Include enzyme dosage, contact time, aeration or oxygen demand, mediator chemicals, pH adjustment, sludge impact, labor, storage losses, and analytical testing. A pilot trial should compare color, phenolic reduction, COD change, toxicity where relevant, and any downstream savings or operational constraints.
Not always. Some substrates are oxidized directly by laccase, while others require a mediator to improve reaction reach or selectivity. For laccase lignin and pulp bleaching projects, test both mediator-free and mediator-assisted conditions. Compare brightness, kappa reduction, lignin modification, chemical savings, effluent load, mediator cost, safety profile, and downstream compatibility before choosing the commercial process.
Pilot validation should use actual plant material and realistic operating conditions. For wastewater, screen pH 4.0-8.5, 25-60°C, relevant contact times, oxygen availability, and dosage bands such as 50-5000 U/L. For pulp or lignin, test solids level, mixing, enzyme charge, mediator need, and reaction time. Measure the business outcome, such as treatment efficiency, bleaching chemical reduction, or lignin functionality.
Related Search Themes
laccase enzyme production from bacteria, laccase enzyme production, laccase enzyme, production and purification of laccase enzyme through fungi, production and industrial applications of laccase enzyme, laccase enzyme production ppt, laccase enzyme production, laccase enzyme production from bacteria
Laccase for Research & Industry
Need Laccase for your lab or production process?
ISO 9001 certified · Food-grade & research-grade · Ships to 80+ countries
Frequently Asked Questions
What is the main difference between laccase enzyme production from fungi and bacteria?
Fungal laccases are often extracellular and widely used in lignin, pulp, dye, and wastewater studies, while bacterial laccases may offer different tolerance profiles for pH, temperature, salinity, or inhibitors. Neither route is automatically better for every plant. Industrial buyers should compare both under real process conditions, including activity retention, impurity profile, dosage, oxygen transfer, mediator requirement, and final treatment result.
What documents should a buyer request before approving a laccase enzyme supplier?
Request a COA, TDS, SDS, assay method, recommended storage conditions, shelf-life data, sample lot number, and pilot trial guidance. The COA should confirm agreed activity, appearance, formulation, and other purchase specifications. The TDS should describe pH, temperature, dosage, compatibility, and inhibitors. The SDS helps site teams evaluate handling, PPE, storage, and spill response before the enzyme enters production.
How should cost-in-use be calculated for laccase wastewater treatment?
Cost-in-use should be calculated per cubic meter treated or per kilogram of pollutant reduction, not only by enzyme purchase price. Include enzyme dosage, contact time, aeration or oxygen demand, mediator chemicals, pH adjustment, sludge impact, labor, storage losses, and analytical testing. A pilot trial should compare color, phenolic reduction, COD change, toxicity where relevant, and any downstream savings or operational constraints.
Does laccase always require a mediator for lignin or pulp applications?
Not always. Some substrates are oxidized directly by laccase, while others require a mediator to improve reaction reach or selectivity. For laccase lignin and pulp bleaching projects, test both mediator-free and mediator-assisted conditions. Compare brightness, kappa reduction, lignin modification, chemical savings, effluent load, mediator cost, safety profile, and downstream compatibility before choosing the commercial process.
What pilot conditions are useful for laccase enzyme production evaluation?
Pilot validation should use actual plant material and realistic operating conditions. For wastewater, screen pH 4.0-8.5, 25-60°C, relevant contact times, oxygen availability, and dosage bands such as 50-5000 U/L. For pulp or lignin, test solids level, mixing, enzyme charge, mediator need, and reaction time. Measure the business outcome, such as treatment efficiency, bleaching chemical reduction, or lignin functionality.
Wholesale Laccase Supply: Request a Quote
For manufacturers, distributors and treatment contractors: send the application, quantity and destination for a wholesale quote. Request a laccase specification review and pilot sample plan for your industrial process. See our application page for Laccase for Industrial Oxidation Jobs at /applications/laccase-enzyme-price-india/ for specs, MOQ, and a free 50 g sample.
Contact Us to Contributehello@mail.enzymemission.com